

A lot of solid polyurethane scrap is created before anyone touches a mold. It comes from the method choice: whether to mix every component in one pass, or to stop halfway and build a controlled intermediate first. For dense, load-bearing elastomers, the answer is usually the second route. That route is the prepolymer method.

Qué es el método de prepolímero
The prepolymer method splits polyurethane chemistry into two stages. In the first, a polyol — polyether or polyester — reacts with an excess of diisocyanate, typically TDI or MDI. The reaction happens in a heated, stirred, vacuum-rated reactor until the mixture becomes an isocyanate-terminated prepolymer with a measured free NCO content. That number, reported as %NCO, is the most important quality marker of the intermediate [1][2].
In the second stage, the prepolymer is mixed with a chain extender immediately before the material enters the mold. The two most common curatives in cast elastomer work are MOCA (4,4′-methylenebis(2-chloroaniline) and 1,4-butanediol (BDO). The mixing ratio is narrow — typically 100 parts prepolymer to 9–12 parts MOCA, or 3–6 parts BDO by weight — because the stoichiometry was already fixed when the prepolymer was made.
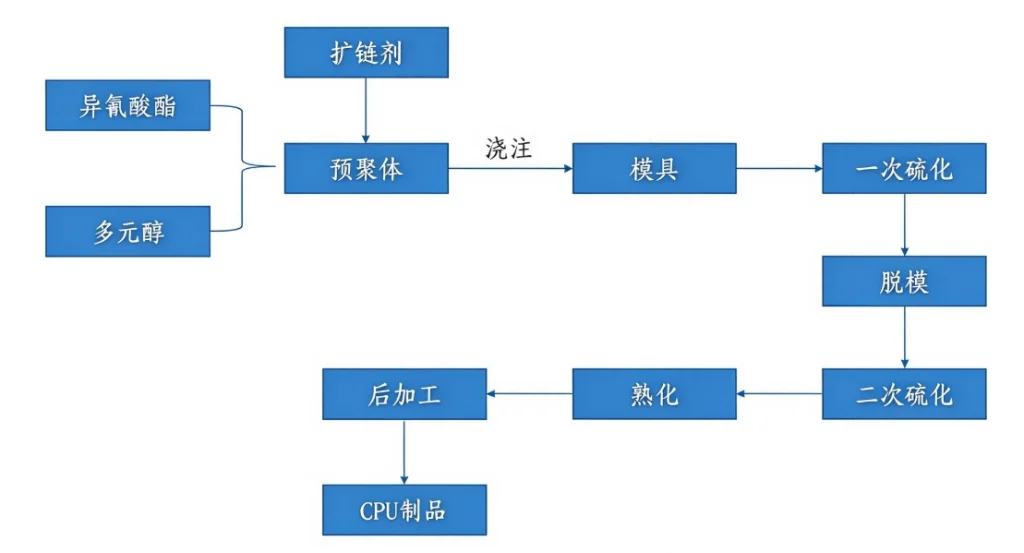
The value of the extra step is control. Part of the reaction exotherm is released in the reactor, so the casting step runs cooler and the pot life is easier to manage. The prepolymer arrives at the machine with viscosity and NCO content already fixed, so the metering and mixing task is repeatable. Free monomer exposure during casting is lower than with direct TDI or MDI addition, because most of the isocyanate has already reacted into the prepolymer.
A one-shot system, by contrast, meters the polyol, isocyanate, catalyst, and chain extender together in a single mix. It works for many foams because the blowing reaction builds viscosity and structure quickly. For solid elastomers, one-shot leaves less room to control hard-segment formation, and it concentrates most of the reaction heat in the mold. That is why the prepolymer route dominates cast polyurethane rather than foaming.
Síntesis del prepolímero: contenido de NCO, desgasificación y almacenamiento
A cast part’s quality is usually decided before the material reaches the casting machine. What happens in the reactor and the day tank sets the floor for everything downstream.
The first control point is %NCO. TDI-based cast prepolymers commonly sit in the 3–6% NCO range, while MDI-based systems can run higher. The number matters because it fixes how much curative the casting machine must add to reach the target stoichiometry. A higher %NCO requires a proportionally larger curative addition; a lower %NCO leaves less margin for error in the ratio. Standard methods determine NCO content by titration or equivalent methods [1][2].
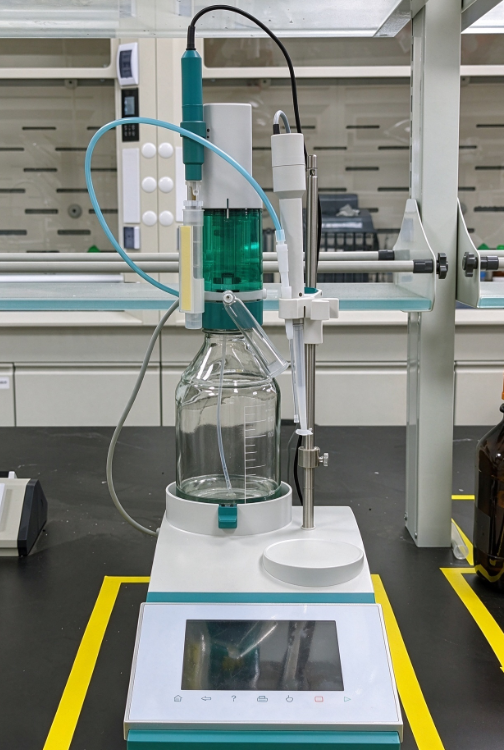
The second control point is moisture. Water reacts with free isocyanate to form carbon dioxide and urea. In a solid casting, that means bubbles and hard, brittle urea domains. Prepolymer synthesis therefore runs under vacuum — commonly below -0.095 MPa — with low-speed stirring and working temperatures between 80°C and 120°C. After synthesis, the prepolymer is stored in heated day tanks, typically 30–80°C, under dry air or nitrogen to keep atmospheric moisture out.
Storage temperature is not arbitrary. It is set low enough to slow side reactions and protect the NCO content, but high enough to keep viscosity pumpable. If the prepolymer cools too far, it thickens and the gear pumps have to work against a rising pressure drop. If it is held too hot for too long, NCO content drifts and the mix ratio stops matching the recipe.
La etapa de colado: endurecedores, estequiometría y vida útil de la mezcla
Establezca las temperaturas de fusión, mantenimiento y línea caliente del MOCA a partir de la TDS/SDS del grado real y de la receta de prepolímero aprobada. Confirme el suministro totalmente líquido en todo el recorrido del material. Un rango nominal de ajuste de la máquina de 90–115 °C no garantiza que todos los grados de MOCA estén fundidos en todo ese rango. Configure el BDO y otros endurecedores según sus propios requisitos de material, dentro de la capacidad nominal del equipo.
Stoichiometry is the lever that tunes hardness. Cast elastomers are typically formulated at 90–100% of theoretical NCO consumption. Running closer to 100% tends to raise hardness and crosslink density; pulling back softens the part and extends the working time slightly. The target Shore hardness then steers the choice of hard-segment content and curative ratio [3].
Pot life sets the pace of the line. Once prepolymer and curative meet in the mixing head, the mixture must be dispensed into the mold before viscosity climbs too far. Fast MOCA systems at higher temperatures can be workable for only a minute or two. BDO systems generally give several minutes. Machine design follows from this: gear-pump metering with dynamic accuracy inside ±0.3%, a high-shear mixing head running roughly 6000–12000 rpm, and a short mixed-material path from head to mold.
One operator-safety point belongs here. MOCA is classified as a carcinogen under the CLP regulation [4]. Handling requires proper ventilation, protective clothing, and closed transfer wherever possible. The same heating that keeps MOCA liquid also makes exposure control a process requirement, not a formality.
Hardness targets are usually the first thing a formulator adjusts, and the choice ripples into curative ratio, mixed viscosity, and demold time. Dureza Shore A frente a Shore D en poliuretano covers how durometer selection changes the formulation and part behavior.
Dónde se usa el método — y dónde no
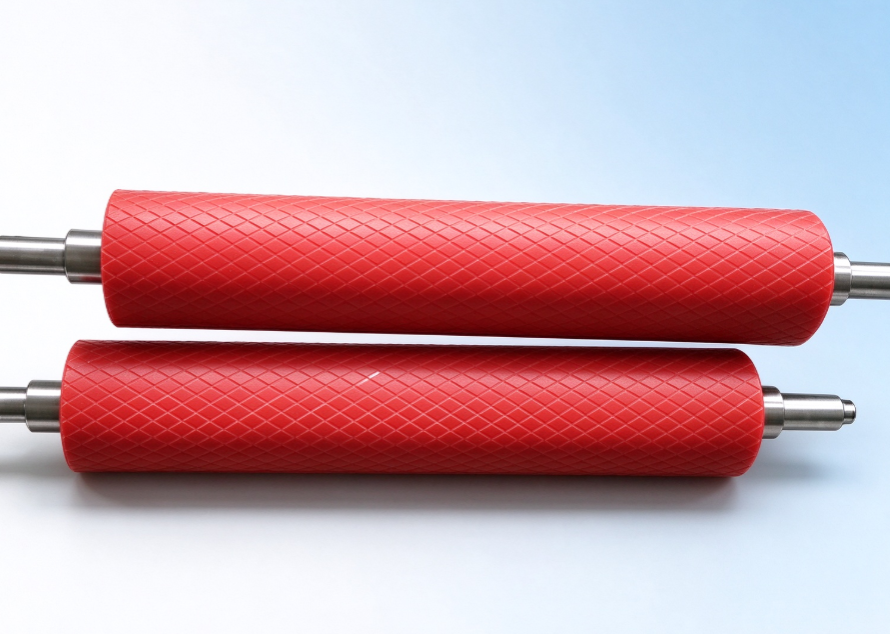
The prepolymer method earns its keep on dense, solid elastomers: printing and industrial rollers, wheels and casters, hydraulic and industrial seals, mining screen plates, rail pads, and automotive suspension buffer blocks. These parts carry load, need Shore A 30–95 hardness, and depend on tear and abrasion resistance that starts with hard-segment control.
The boundary is not rigid, but it is useful. Low-density flexible and rigid foams generally stay with one-shot because a high-functionality polyol, a blowing agent, and a fast catalyst can build the full structure in one pass. Solid elastomers move toward the prepolymer route because there is no blowing reaction to carry the extra control burden.
Rail pads are a practical example. Their job is to hold elastic modulus and dimensional accuracy within tight limits over millions of load cycles, and tests under standards such as EN 13146 punish any drift in cure or hardness [5]. A line casting solid elastomer wheels faces the same logic in a different shape: ±0.3% metering accuracy usually matters more than a larger nominal throughput, because a one-percentage-point ratio shift moves hardness and cure enough to create soft spots and scrap.
Roller casting is one of the clearest cases for the prepolymer route, because the cure profile and hardness uniformity decide whether a roller survives contact pressure and keeps its dimensions. Cómo se fabrican los rodillos de poliuretano, desde la colada hasta el curado covers the casting-to-cure sequence that protects that uniformity.
If you are comparing a prepolymer reactor and a casting machine for a solid-elastomer line, send your part weight, target hardness, and curative type to info@chinahaifeng.com. Those three numbers determine tank sizing, heating capacity, and whether the mixing head needs MOCA/BDO switching. The inquiry checklist at the end of this article spells out the full list.
Lista de verificación para la selección de equipos en líneas de prepolímero
When the method is set, the equipment list follows from the chemistry. The items below are the ones that most often decide whether a start-up or upgrade stays stable.
- Reactor capacity — sized to your batch and NCO target, with vacuum capability below -0.095 MPa, heating to 80–120°C, and low-speed stirring for uniform synthesis.
- Establezca las temperaturas de fusión, mantenimiento y línea caliente del MOCA a partir de la TDS/SDS del grado real y de la receta de prepolímero aprobada. Confirme el suministro totalmente líquido en todo el recorrido del material. Un rango nominal de ajuste de la máquina de 90–115 °C no garantiza que todos los grados de MOCA estén fundidos en todo ese rango. Configure el BDO y otros endurecedores según sus propios requisitos de material, dentro de la capacidad nominal del equipo.
- Precisión de dosificación — gear pumps with dynamic accuracy inside ±0.3% across the full flow range, not just at the midpoint where brochures quote it.
- Cabezal de mezcla — high-shear in the 6000–12000 rpm range, with a short path to the mold and automatic solvent or air purge to prevent cured material from blocking the chamber between shots.
- Vacuum defoaming — applied to the prepolymer before and during holding, not only to the day tank, so dissolved gas does not become part porosity.
- Formula switching — if you run MOCA and BDO on the same line, one-click recipe storage and clean purge matter more than raw speed.
Metering accuracy matters most when shot weights are small, because a fixed percentage error turns into a large gram error on a 50–500 g part. Cómo calcular el peso de dosificación en poliuretano covers how to size the shot and check the dosing range before you buy.
Denos sus datos de proceso, no solo el producto
For a prepolymer-method line, the most useful inquiry includes more than a model number request. Send the process data that shapes the equipment:
- Part weight (or shot weight) and required output per hour
- Prepolymer NCO content and viscosity at process temperature
- Curative type — MOCA, BDO, or another chain extender — and target Shore hardness
- Batch size and vacuum requirements for the reactor
- Whether you need color dosing, wear-resistant additive tanks, or multi-component capability
Send these to info@chinahaifeng.com or WhatsApp 86 13566296633. We size the metering, heating, and mixing around your formula — not the other way around.
Preguntas frecuentes
¿Cuál es la diferencia entre los métodos de una sola etapa y de prepolímero?
One-shot mixes polyol, isocyanate, and chain extender together in a single step. The prepolymer method first reacts polyol with excess isocyanate in a reactor, then mixes the resulting prepolymer with a curative at the machine.
¿Qué le indica el contenido de NCO sobre un prepolímero?
%NCO reports the remaining isocyanate available for chain extension. It fixes the curative addition needed to reach the target stoichiometry, so it directly affects mix ratio, hardness, and pot life [1][2].
¿Qué piezas realmente necesitan el método de prepolímero?
Dense, load-bearing elastomers — rollers, wheels, seals, screen plates, rail pads, and buffer blocks — benefit most. Low-density foams generally stay with one-shot because the blowing reaction provides the needed structure.
¿Puede una sola máquina de colado usar tanto MOCA como BDO?
Establezca las temperaturas de fusión, mantenimiento y línea caliente del MOCA a partir de la TDS/SDS del grado real y de la receta de prepolímero aprobada. Confirme el suministro totalmente líquido en todo el recorrido del material. Un rango nominal de ajuste de la máquina de 90–115 °C no garantiza que todos los grados de MOCA estén fundidos en todo ese rango. Configure el BDO y otros endurecedores según sus propios requisitos de material, dentro de la capacidad nominal del equipo.
¿Por qué se forman burbujas en las piezas de prepolímero?
Water is usually the cause. Moisture reacting with free NCO forms carbon dioxide and urea. The fix is stricter vacuum degassing of the prepolymer, dry-air or nitrogen blanketing, and keeping raw materials dry.
¿Necesito un reactor para usar el método de prepolímero?
A synthesis reactor is needed when the project includes producing the prepolymer. A casting line using a purchased prepolymer can be configured without that synthesis stage. Define the material supply route and process scope before selecting reactor or casting equipment.
Referencias
[1] ISO 14896:2009, Plásticos — Materias primas para poliuretanos — Determinación del contenido de isocianato, International Organization for Standardization.
[2] ASTM D2572-19, Método de ensayo estándar para grupos isocianato en materiales de uretano o prepolímeros, ASTM International.
[3] ISO 48-4:2018, Rubber, vulcanized or thermoplastic — Determination of hardness — Part 4: Indentation hardness by durometer method (Shore hardness), International Organization for Standardization.
[4] Regulation (EC) No 1272/2008 on classification, labelling and packaging of substances and mixtures (CLP), European Union. MOCA (4,4′-methylenebis(2-chloroaniline) classification.
[5] EN 13146, Railway applications — Track — Test methods for fastening systems, European Committee for Standardization.
Si te interesa, echa un vistazo a estos artículos relacionados:
RRIM frente a RIM: qué proceso se adapta mejor a tu pieza estructural
Dureza Shore A frente a Shore D en poliuretano
Qué es la espuma de poliuretano semirrígida
Medición de la resiliencia de la espuma de poliuretano: guía práctica de ensayo
Cómo calcular el peso de dosificación en poliuretano
Specifying hot-cast polyurethane elastomer processing equipment
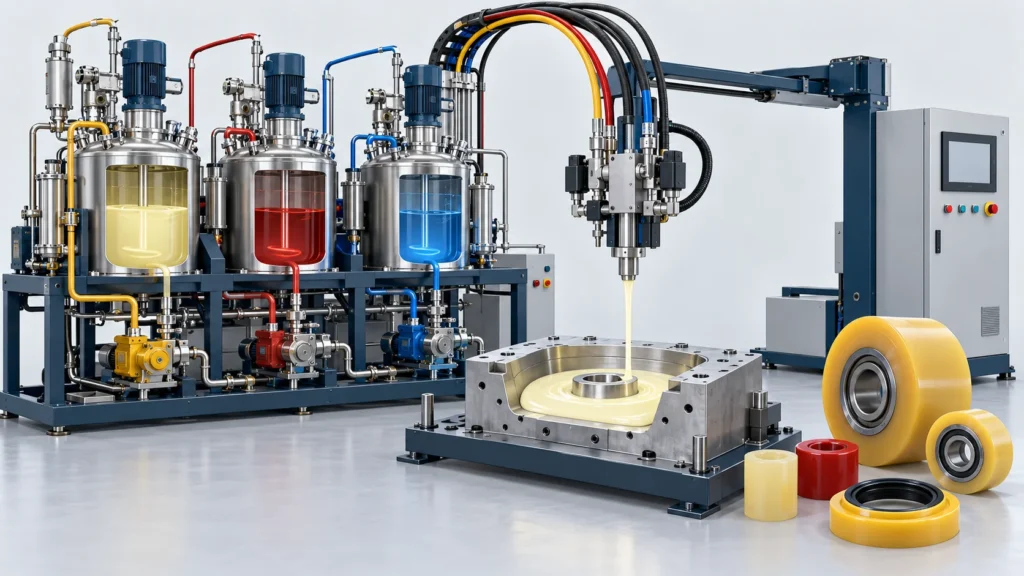
Cast polyurethane elastomers are made by metering a reactive system into tooling and curing the part under its approved process conditions. In hot-cast polyurethane processing, control the material and tool conditions from degassing through mixing, pour, demold and post-cure. The product specification, supplier chemistry and geometry of the cast elastomer establish the process window.
When comparing cast elastomer machinery, request its component count, viscosity range, flow stability at the minimum and maximum pour, and cleaning or changeover procedure. For a cast elastomer trial, use the actual supplied materials and agree hardness, critical dimensions and any compression, abrasion or bonding tests for the application. See industrial elastomer casting plant scope y roller casting production sequence.





