
Proyecto de línea de TPU para película soplada médica en China
Project reference: Medical Blown-Film TPU Line Project. Configuration and reported outcomes require original project records.
Resumen del proyecto
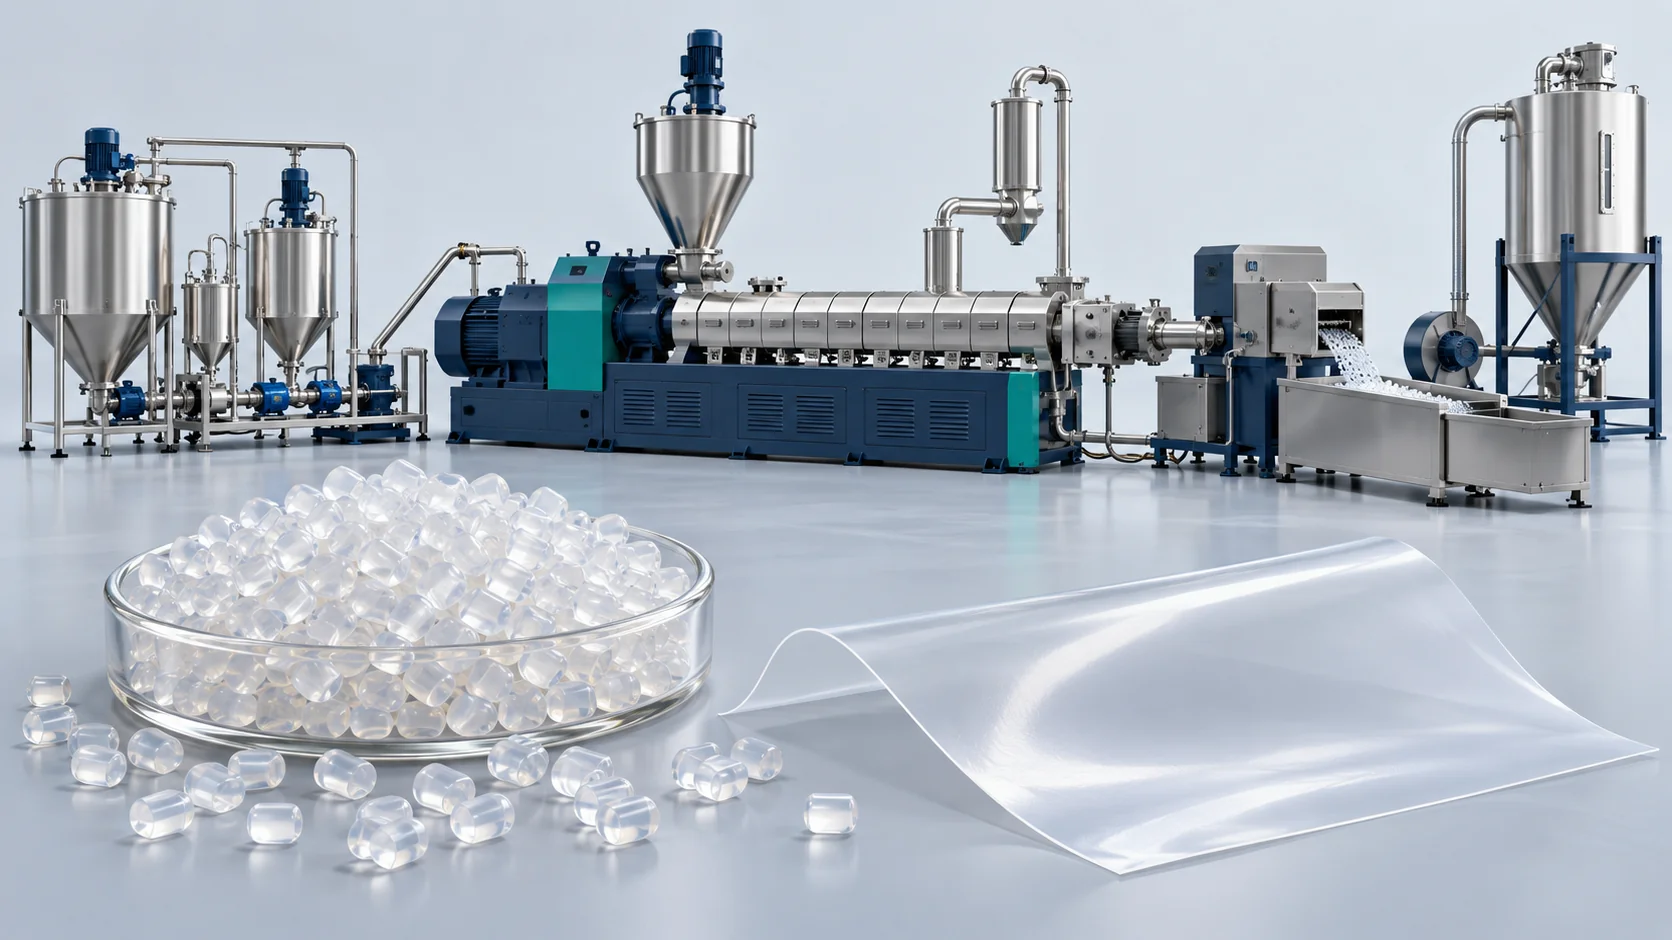
Aviso sobre las ilustraciones. Las ilustraciones del proceso no son fotografías verificadas de esta instalación.
Base de la referencia del proyecto. Las cifras y los detalles de configuración se reportan en el resumen del proyecto suministrado. Son valores de referencia para la aplicación indicada, y no resultados de aceptación verificados ni una garantía para otra instalación. Confirme los registros de origen, el material, el utillaje, el programa de operación y el método de ensayo al evaluar un proyecto comparable.
A leading national technical film and polymer enterprise in Zhejiang deployed Haifeng’s high melt-strength reactive extrusion line. The facility was commissioned to produce ultra-high molecular weight, high-melt-strength thermoplastic polyurethane (TPU) pellets engineered specifically for 15-micron breathable medical surgical drape films.
Prior to this installation, the client relied on standard extrusion-grade TPU resins. Due to low extensional melt viscosities and broad molecular weight distributions (Mn around 70,000), attempts to blow thin 15 µm films resulted in violent bubble oscillation and sagging. Operators suffered frequent bubble ruptures every 6 to 8 hours, causing massive resin scrap. Furthermore, moisture vapor transmission rates (MVTR) plateaued at 4,500 g/(m²·24h), failing export surgical barrier specifications.
Haifeng engineered a turnkey reactive extrusion plant centered on the HF-TPU85-FLM system. Combining four-stream mass flow dosing, an extended L/D = 58 branching twin-screw extruder, and a heavy-duty melt gear pump, the plant synthesized ultra-high molecular weight TPU (Mn ≥ 120,000). The resulting resin ran continuously on downstream blown-film lines for over 72 hours without bubble breaks, producing 15 µm films with an MVTR of 8,250 g/(m²·24h).
Limitaciones de los datos: The document reports 74.5 h uninterrupted operation inside a stated 72 h assessment; the observation duration and aggregation remain unverified. Melt pressure variation is not a guarantee of downstream bubble stability. MVTR varies with film thickness and method. Medical-use suitability is not established by the equipment brief.
Ilustración conceptual: Ilustración conceptual generada para el análisis del proceso; no es una fotografía de la máquina especificada, de una instalación del cliente ni de un proyecto entregado.
Entrega de soluciones
Configuración reportada en el resumen suministrado.
Haifeng engineered an automated reactive compounding plant optimized for high-molecular-weight synthesis. High-purity hydrophilic polyether polyols, pure molten MDI, 1,4-BDO, and long-chain branching curatives are conditioned in stainless steel day tanks under nitrogen blankets at 80°C.
The components are metered into Zone 1 of an L/D = 58 co-rotating twin-screw extruder using Coriolis-guided servo pumps. Across 14 independently regulated barrel zones, gentle distributive mixing blocks build an ultra-high molecular weight matrix (Mn = 125,000) through controlled branching reactions, holding processing exotherms under tight limits.
An oil-jacketed melt gear pump pulls polymer from screw tips, maintaining steady discharge pressure at 15.2 MPa into a 325-mesh continuous screen changer with pressure drift held within ±0.03 MPa. The melt extrudes through multi-orifice die plates into a tempered water cutting chamber, sliced into uniform spherical pellets by carbide knives. After centrifugal de-watering to < 0.02% moisture, the resin feeds into cleanroom blown-film lines, delivering flawless 15 µm bubble stability across 72 continuous operating hours.
The document reports 74.5 h uninterrupted operation inside a stated 72 h assessment; the observation duration and aggregation remain unverified. Melt pressure variation is not a guarantee of downstream bubble stability. MVTR varies with film thickness and method. Medical-use suitability is not established by the equipment brief.
| Equipos | Modelo | Cant. | Función |
|---|---|---|---|
| High Melt-Strength TPU Extruder | HF-TPU85-FLM (L/D = 58) | 1 unidad | Core continuous long-chain branching reaction and 0.02 kPa vacuum de-volatilization. |
| Jacketed High-Torque Melt Gear Pump | HF-MGP-150 | 1 unidad | Pressure decoupling holding die discharge fluctuations within ±0.03 MPa. |
| Four-Stream Mass-Flow Dosing Skid | HF-LDS-04M | 1 unidad | Continuous servo metering with Coriolis mass tracking for branching agents. |
| Enclosed Underwater Pelletizer Skid | HF-UWP-800M | 1 unidad | Die-face hot cutting, spin drying to < 0.02% moisture, and packaging. |
Familias de equipos relacionados
Las referencias del catálogo describen familias de equipos relacionados. El modelo entregado, los equipos auxiliares y las condiciones de aceptación se rigen por la configuración del proyecto.
Resultados reportados — se requieren los registros originales
Master High Melt-Strength Blown-Film TPU Production
Comparta su aplicación, sistema de materiales, producción objetivo y condiciones de la fábrica. Nuestro equipo le responderá en un día hábil. Una vez aclarados los requisitos, le proporcionamos una propuesta preliminar en un plazo de dos días hábiles.


