
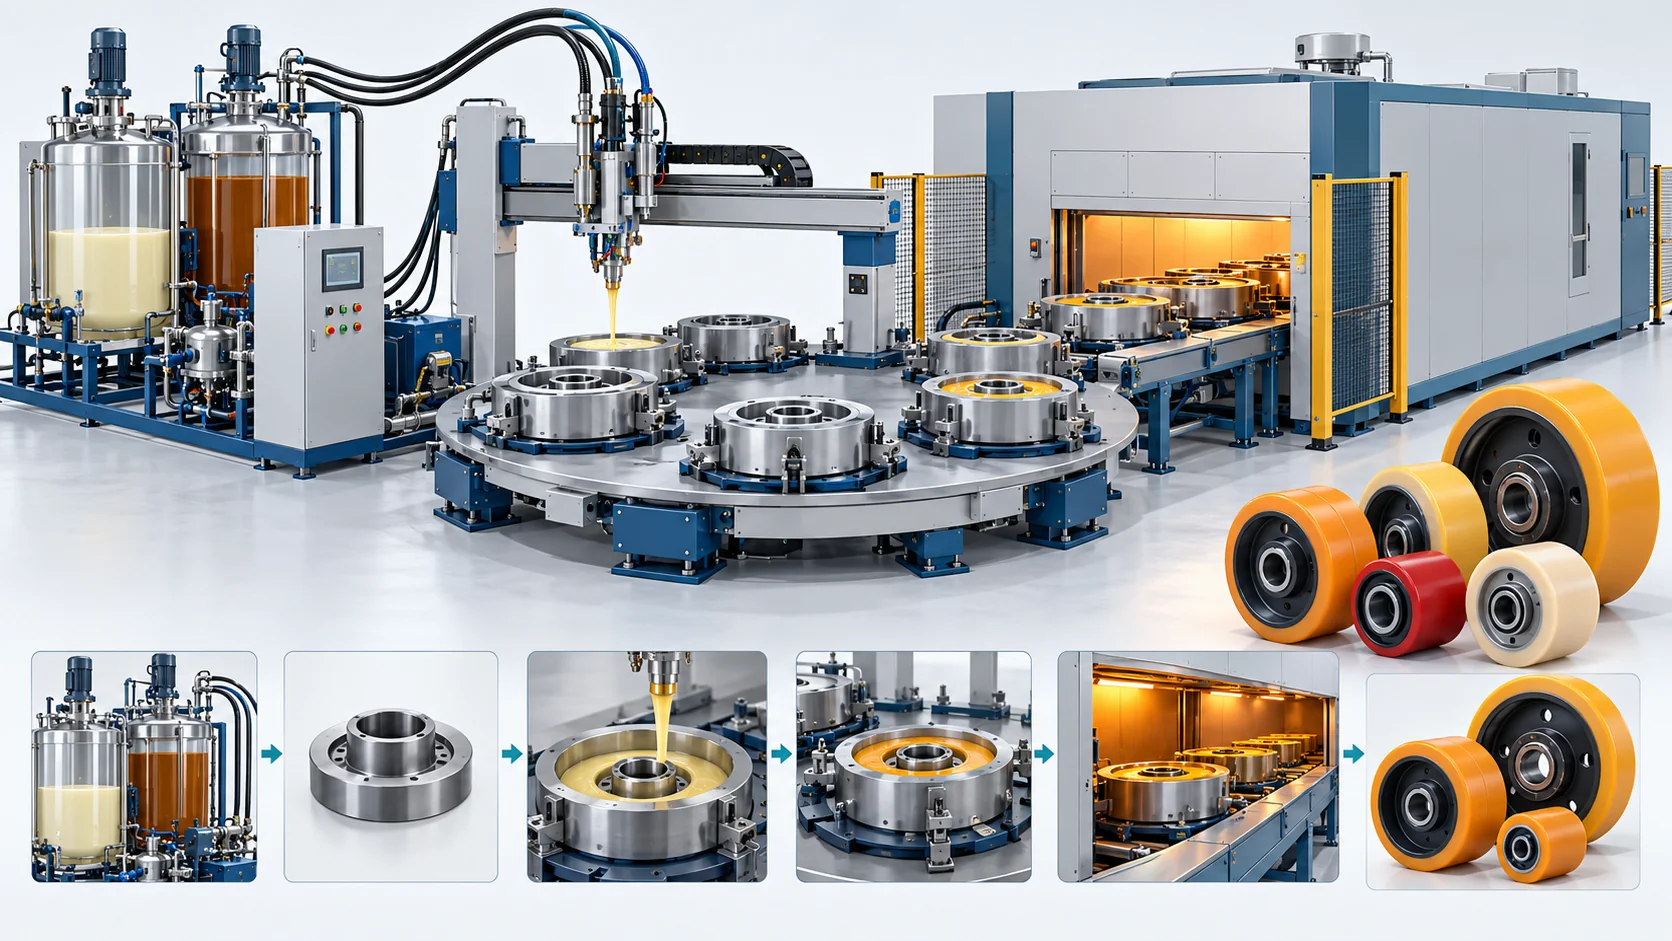
خط صب عجلات PU الأوتوماتيكي | عجلات AGV والرافعات الشوكية
إنتاج مُهيَّأ لعجلات البولي يوريثان الصلبة، يشمل واجهات تجهيز القلب والتسخين المسبق بالحث والتوزيع ثنائي التدفق والمعالجة في قوالب مُفهرسة.
معدل تدفق التصريف
2.0 to 18.0 kg/min (Dual-flow matrix switching)
نسبة الخلط
100:8 to 100:25 (By weight)
مرجع الدقة
±0.2% (Continuous closed-loop Coriolis feedback)
Core Preheating Reference
90°C ±2°C metal-core preheating
High-Bonding Automated Polyurethane Solid Wheel Casting
إنتاج مُهيَّأ لعجلات البولي يوريثان الصلبة، يشمل واجهات تجهيز القلب والتسخين المسبق بالحث والتوزيع ثنائي التدفق والمعالجة في قوالب مُفهرسة.
إنتاج مُهيَّأ لعجلات البولي يوريثان الصلبة، يشمل واجهات تجهيز القلب والتسخين المسبق بالحث والتوزيع ثنائي التدفق والمعالجة في قوالب مُفهرسة.
تشمل الحزمة تحضير المواد، والخلط الديناميكي ثنائي التدفق، والتسخين المسبق لصرة العجلة بالحث، وخط القوالب المُسخّن المحدد ووحدات التحكم. وتُعدّ عمليات السفع/التنظيف الآلية وفك القوالب الهيدروليكي اختيارية. تُوَرَّد مادة البوليمر الأولي وعوامل الترابط بشكل منفصل؛ أما طاقة الموقع والهواء المضغوط فهي واجهات يتحملها العميل. وتعتمد الطاقة الإنتاجية على عدد مواضع القوالب المتوازية ومراحل الدورة وحجم المنتج.
تدفق المواد ومبدأ العمل
Core Surface Abrasive Blasting & Bonding Adhesive Application
Forged steel or ductile iron wheel cores are automatically grit-blasted to Sa 2.5 cleanliness and spray-coated with Chemlok bonding primer before entering a drying tunnel.
Medium-Frequency Induction Core Preheating
Primed wheel cores pass through a medium-frequency induction heating coil, bringing metal core temperatures rapidly to 90°C ± 2°C in 45 seconds to activate the bonding adhesive.
High-Accuracy Servo Polyurethane Metering
High-precision servo-driven gear pumps measure MDI prepolymer and 1,4-BDO chain extender under continuous Coriolis mass flow control, maintaining mix ratios within ±0.2%.
Dual-Flow Matrix Dynamic Dispensing
Material enters the dual-flow mixing head; a low-flow nozzle injects 3 kg/min into the narrow hub clearance to displace air, before the main nozzle floods the tire tread cavity at 15 kg/min.
In-Mold Pressurized Curing & Conveyance
Filled wheel molds travel along a heated 100°C closed-loop indexing conveyor, achieving demold green strength in 15 minutes before automated hydraulic extraction and post-curing.
هل تحتاج إلى عرض سعر لهذه المعدات؟
اطلب عرض سعرالطراز والمعايير الفنية
Configuration values from the supplied HF-CPU180-WL brief. Final performance is confirmed for the chemical formulation, tool, operating conditions and original calibration records. Casting-circuit pressure is distinct from finished-component service or qualification pressure.
| المعلمة الفنية | HF-CPU180-WL |
|---|---|
| المكوّنات | 2 Primary Streams (A: Prepolymer, B: Curative) + 1 Color/Additive |
| نطاق الإخراج | 2.0 to 18.0 kg/min (Dual-flow matrix switching) |
| نطاق نسبة الخلط | 100:8 to 100:25 (By weight) |
| مرجع الدقة | ±0.2% (Continuous closed-loop Coriolis feedback) |
| مصدر الطاقة | 380 فولت، ثلاثي الأطوار، 50 هرتز (اختياري مخصص 440 فولت/480 فولت 60 هرتز) |
| ضغط التشغيل | 0.3 to 0.7 MPa (Metering lines and dynamic head) |
| سعة الخزان / القادوس | Tank A: 200 L (Oil-jacketed), Tank B: 80 L (Stainless steel) |
| الوزن | 4,200 kg (Main casting unit and induction heater) |
| الأبعاد (الطول×العرض×الارتفاع) | 3200 mm x 2100 mm x 2400 mm |
| Induction Preheating Cycle | 45 seconds (To reach 90°C ± 2°C); Medium-frequency induction coil |
| Single-Wheel Molding Tact Time | ≤ 90 seconds (For Ø 300 mm solid wheel); Dual-flow matrix injection |
| Interfacial Peel Adhesion | > 30 kN/m (Polyurethane to metal core); ASTM D429 Method B 90° peel |
| Dynamic Rolling Temperature | ≤ 45°C (Continuous 25 km/h at 3-ton load); Drum endurance test bed |
الميزات الرئيسية للمعدات
تشمل الحزمة تحضير المواد، والخلط الديناميكي ثنائي التدفق، والتسخين المسبق لصرة العجلة بالحث، وخط القوالب المُسخّن المحدد ووحدات التحكم. وتُعدّ عمليات السفع/التنظيف الآلية وفك القوالب الهيدروليكي اختيارية. تُوَرَّد مادة البوليمر الأولي وعوامل الترابط بشكل منفصل؛ أما طاقة الموقع والهواء المضغوط فهي واجهات يتحملها العميل. وتعتمد الطاقة الإنتاجية على عدد مواضع القوالب المتوازية ومراحل الدورة وحجم المنتج.
Hub Induction Preheating
The specified induction stage conditions the metal hub; adhesive selection and actual bonding performance require validation.
Dual-Flow Dispensing
Programmed leading and main-fill rates are selected for hub clearance and tread cavity geometry.
Material and Endurance Testing
Rolling heat and bond durability are verified for wheel size, compound, load and speed rather than inferred from the dispenser.
Indexed Production Interfaces
Mold indexing and curing can operate in parallel. Total output requires a complete line balance and operating record.
ناقش تكوين معداتك
شارك معلومات منتجك والمواد والتجهيزات القالبية ومتطلبات الإنتاج كي نتمكن من مراجعة المعدات والواجهات لمشروعك.
الأسئلة الشائعة
How are hub preheating and bonding targets validated?
How does dispensing time differ from in-mold curing time?
How are wheel rolling temperature and durability verified?
How is the complete wheel-line shift output established?
هل أنت مستعد لمناقشة مشروعك؟
تواصل مع فريقنا


