
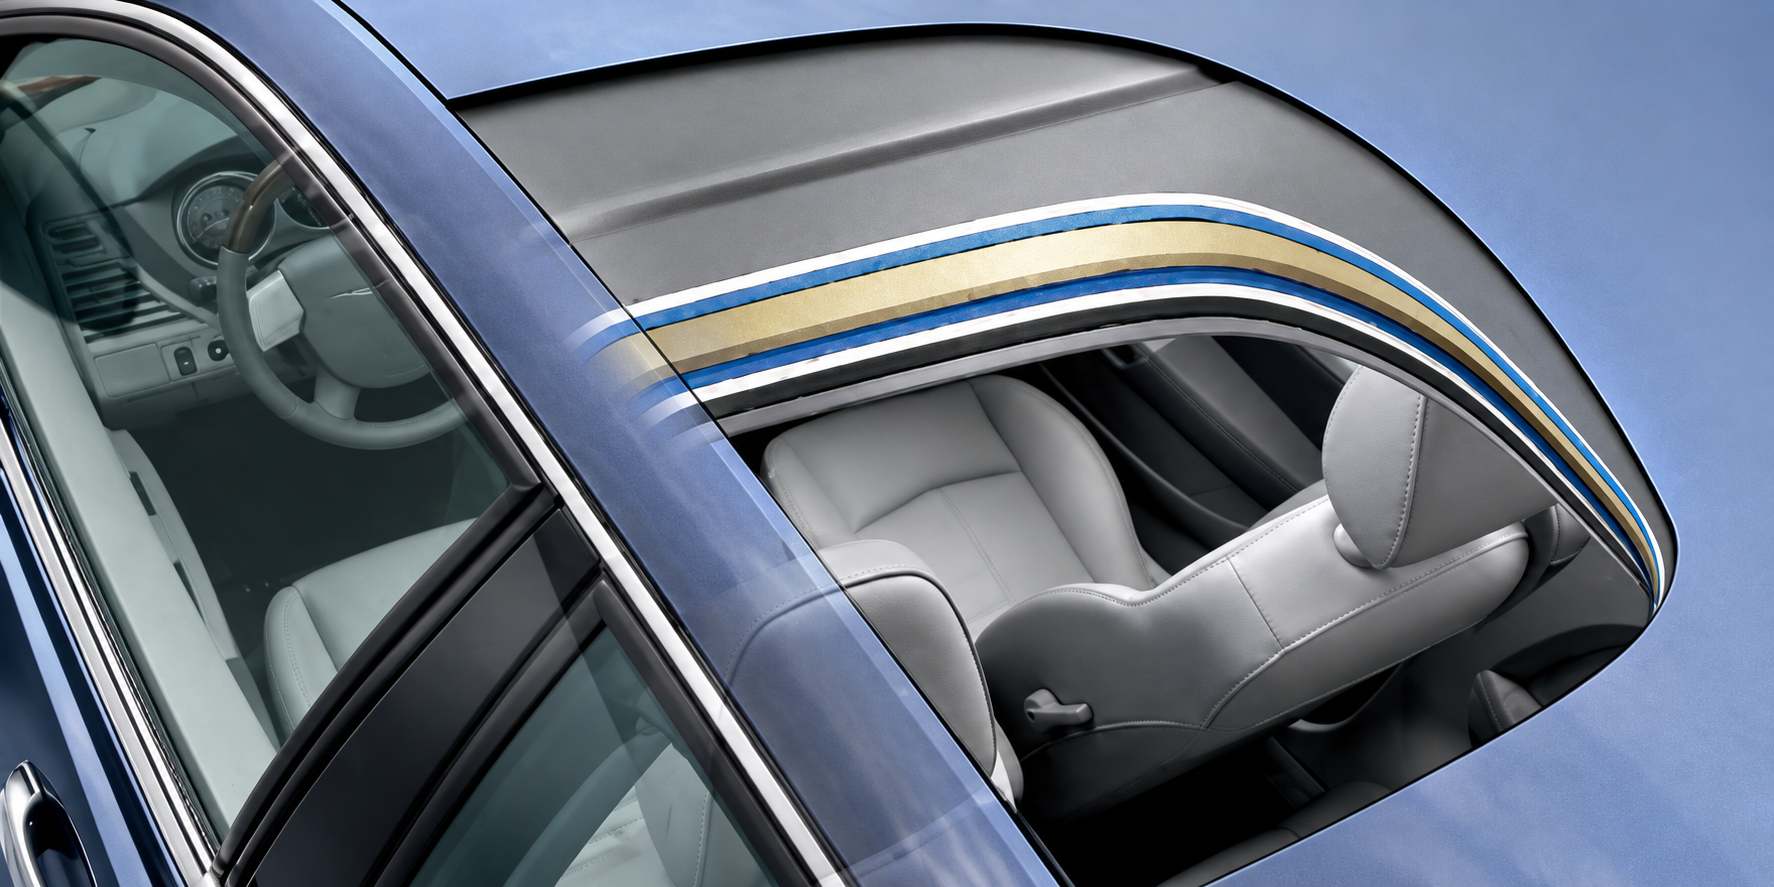
حل الرغونة الصندوقية لسقف المركبات الداخلي
Traditional low-pressure box foaming for semi-rigid automotive headliner blanks, followed by curing, precision slicing and optional lamination.
Box Foaming and Slicing for Automotive Headliner Blanks
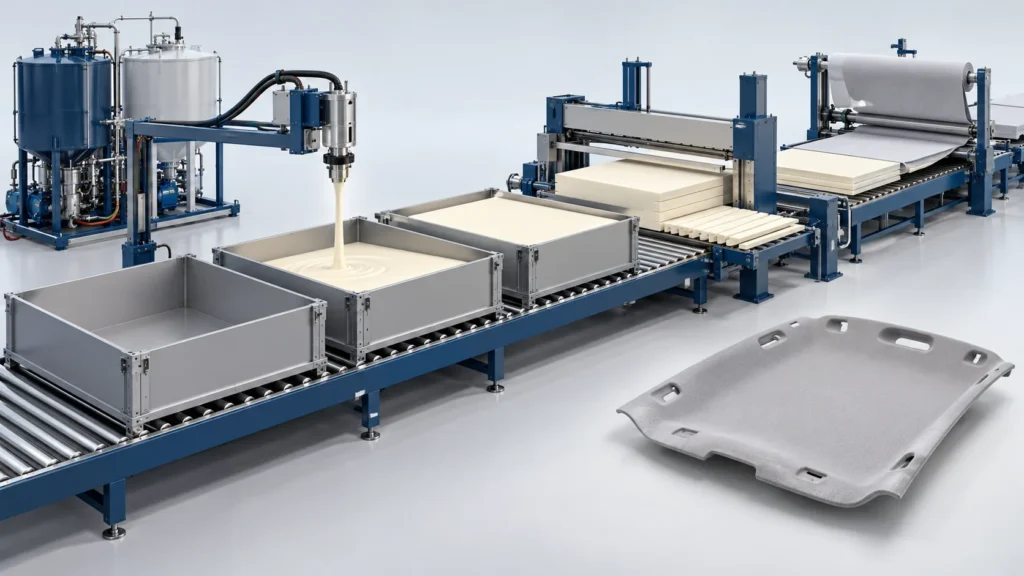
This headliner route starts with traditional low-pressure polyurethane box foaming. Polyol and isocyanate are metered and dynamically mixed, then poured into a box mold where the semi-rigid foam rises. After curing and conditioning, the foam block is sliced into blanks for acoustic and flame-retardant headliner applications. Lamination and thermoforming are separate downstream operations. The supplied project targets a cured foam density of 22 kg/m³ and low-emission interior panels.
Controlled Semi-Rigid Box Foam
Low-pressure metering and dynamic mixing support uniform rise and repeatable density across each box-foamed block.
Acoustic and Low-Emission Blanks
Cured blocks are sliced to panel thickness before optional lamination, with formulation selected for acoustic, flame-retardant and VOC targets.
Define the intermediate foam block and sheet needed by the headliner operation. Block foaming, conditioning, slicing, lamination and subsequent heated forming are separate duties; specify transfer and quality criteria at each handover.
Low-Pressure Box Foaming and Headliner Blank Workflow
Four stages separate foam block production from downstream headliner forming.
Condition and Meter Raw Materials
Condition polyol and isocyanate, then meter the recipe through the low-pressure foaming unit.
Dynamic Mix and Box Pour
A mechanical mixing head blends the components and dispenses the mix into the open box mold.
Free Rise, Cure and Condition
The foam rises in the box; the block is then cured and conditioned before cutting. Time depends on the formulation and block size.
المواصفات الهندسية والمعلمات الفنية
The 70-second figure refers to downstream press work in the supplied project, not box-foam demolding.
| المعلمة الفنية | Specification / Value | Engineering Context |
|---|---|---|
| التطبيق المستهدف | Automotive headliner and roof acoustic blanks | Semi-rigid foam blocks cut to panel thickness |
| Core Process | Low-pressure metering, dynamic mixing and box foaming | Free-rise foam is cured before slicing |
| مصفوفة المواد | Semi-rigid, low-density polyurethane foam | Recipe selected for acoustic and flame-retardant requirements |
| نطاق كثافة الرغوة | 20–30 kg/m³; project target 22 kg/m³ | Confirm density across the cured block |
| قياس الجرعات والخلط | Low-pressure dispensing with dynamic mechanical mixing | Output and mix speed configured to the box size and recipe |
| Block Conditioning | Cure and age before precision slicing | Cure time depends on formulation and block dimensions |
| دورة الكبس في المرحلة اللاحقة | 70 s in the supplied project | Thermoforming/lamination stage; not box-foam demolding time |
| Air Quality | VDA 278 tested in the supplied project | Low-emission formulation and downstream panel validation |
| نطاق التوريد | Low-pressure foaming unit, temperature control and PLC | Box molds, slicing and press interfaces configured by project |
معدات Haifeng ذات الصلة
The general low-pressure reference supports selected block-foaming duties. Cutting and downstream headliner lamination/forming require their own equipment scope.
المزايا الهندسية الرئيسية
For Low-Pressure PU Box Foam for Automotive Headliners, assess material compatibility, process control, equipment interfaces and changeover needs against your production brief.
22 kg/m³ Project Foam Density
Semi-rigid foam block density is controlled before slicing into lightweight headliner blanks.
Low-Emission Material Route
The supplied project uses a formulation evaluated for automotive interior VOC requirements.
Traditional Box-Foam Process
Low-pressure dynamic mixing and free-rise box foaming create blocks for subsequent curing and cutting.
Cut-to-Thickness Flexibility
Cured foam blocks can be sliced to different blank thicknesses before downstream lamination.
مشاريع ذات صلة
Use the linked headliner project for its documented block/sheet and downstream interfaces; material emissions results stay tied to the reported specimen.
الأسئلة الشائعة
أسئلة هندسية وشرائية حول مسار إنتاج البولي يوريثان هذا.
Is this headliner process high-pressure injection molding?
When are headliner blanks sliced?
Does the 70-second figure describe box-foam demolding?
كيف يختلف الإنتاج بالصب في القوالب عن الإنتاج المستمر للكتل الرغوية (Slabstock)؟
ما المدخلات اللازمة لهذا التكوين؟
Where does the box-foaming package end in headliner production?
ناقش مشروع الإنتاج الخاص بك في قطاع السيارات
Share the following for this application: Formulation, foam-block geometry, density target, conditioning instructions, required sheet thickness, cutting demand and downstream laminate. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


