
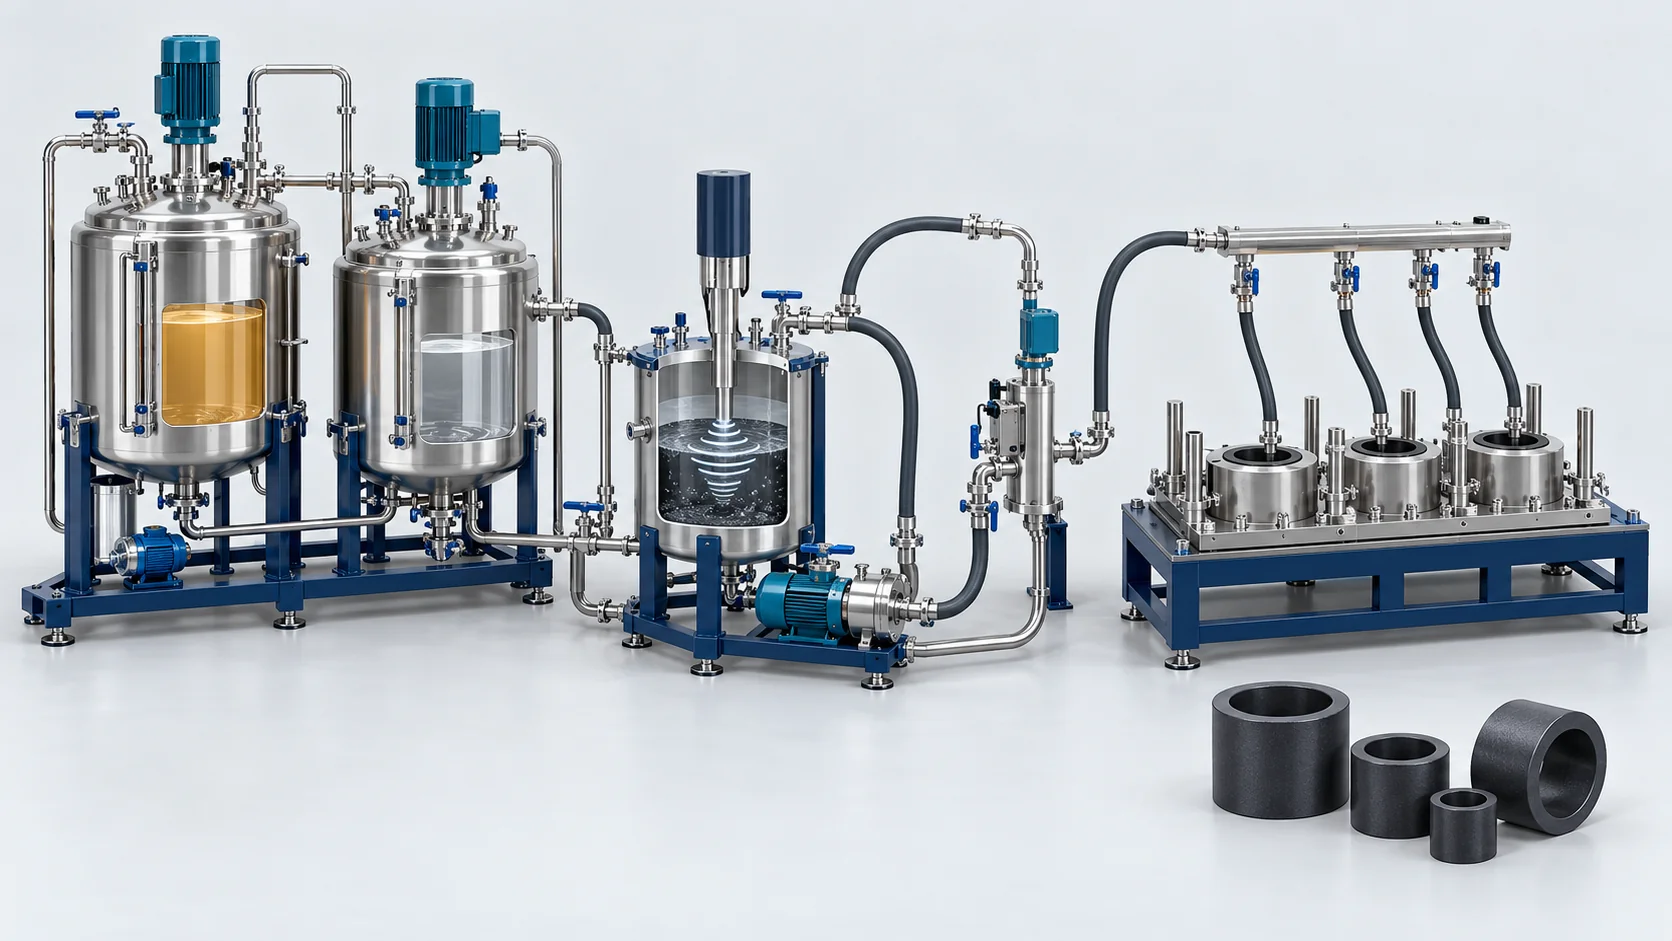
Solución de fundición de nailon MC modificado con MoS2
Configure additive dispersion, circulation and reactive MC Nylon casting for the selected modified bushing material.
Wear and Lubrication Process Engineering for Heavy Machinery Bearings
Modified nylon bushing production requires additive wetting, dispersion, suspension control and a compatible reactive casting process. Ultrasonic frequency and pump construction describe equipment functions; they do not establish friction coefficient, wear life or maintenance-free service for a bushing.
Alcance de suministro definido
Define additive preparation, thermal holding, recirculation, metering and tooling together. Powder size terminology must follow the actual distribution rather than treating micron-sized powder as submicron.
Insumos para la selección del proceso
Powder distribution/loading, monomer data, batch hold, bushing drawing, counterface, load/speed and exposure.
Equipment scope, retained factory interfaces and acceptance are agreed for the selected material and part. Define additive preparation, thermal holding, recirculation, metering and tooling together. Powder size terminology must follow the actual distribution rather than treating micron-sized powder as submicron.
MoS2-Modified MC Nylon Casting Workflow
Characterize the formulation → Disperse and circulate → Meter and cast → Condition and evaluate. Define preparation, filling, cure and output timing separately for the selected configuration.
Characterize the formulation
Confirm monomer system, MoS2 size/loading and any other additive.
Disperse and circulate
Develop the wetting, dispersion and hold procedure for the actual powder.
Dosificar y colar
Validate material delivery and reaction in the selected bushing tool.
Envolvente de ingeniería de la solución de referencia
Configuración existente y referencias de ensayo. Los ajustes del equipo, los resultados del material y los resultados del conjunto terminado son independientes; aplique cada valor solo a su configuración y condiciones documentadas.
| Parámetro | Valor / Unidad | Configuración / Condiciones aplicables |
|---|---|---|
| Continuous Casting Flow Rate | 3.0 to 25.0 kg/min | Zirconia ceramic-lined positive displacement pump skid |
| Dynamic Friction Coefficient | 0.08 to 0.12 (Dry unlubricated friction) | ASTM G99 pin-on-disk test under 35 MPa contact pressure |
| Ultrasonic Cavitation Frequency | 20 kHz (Continuous acoustic horn) | High-power ultrasonic generator inside molten vessel |
| Supported MoS₂ Powder Loading | 1.0% to 6.0% by weight | Sub-micron 1– 3 µm particle size de-agglomerated |
| Grease-Free Bushing Wear Life | Greater than or equal to 8,000 Hours | Verified radial wear under 0.1 mm in abrasive dust service |
| Annealing Oil Bath Temperature | Up to 150°C | Multi-zone thermal oil immersion tank relieving stress |
Equipos principales de esta solución
Las referencias de equipos se seleccionan según su proceso documentado. La dosificación principal, el suministro auxiliar y las rutas alternativas no constituyen un único paquete estándar.
Controles de proceso y verificaciones de aplicación
Evalúe estas funciones con el material, los moldes y el resumen de producción seleccionados. Los resultados de las piezas acabadas requieren su propia evidencia de aceptación.
Additive-specific preparation
Select dispersion and circulation after material trials and endpoint evaluation.
Compatible material circuits
Review filled-material wear, seals, thermal control and cleaning.
Duty-specific tribology
Separate equipment functions from friction and endurance measurements.
Proyectos relacionados
Estas son referencias de aplicación relacionadas. Compare el material, el proceso y los módulos entregados reales; las cifras de proyecto reportadas no son resultados de aceptación para otra línea.
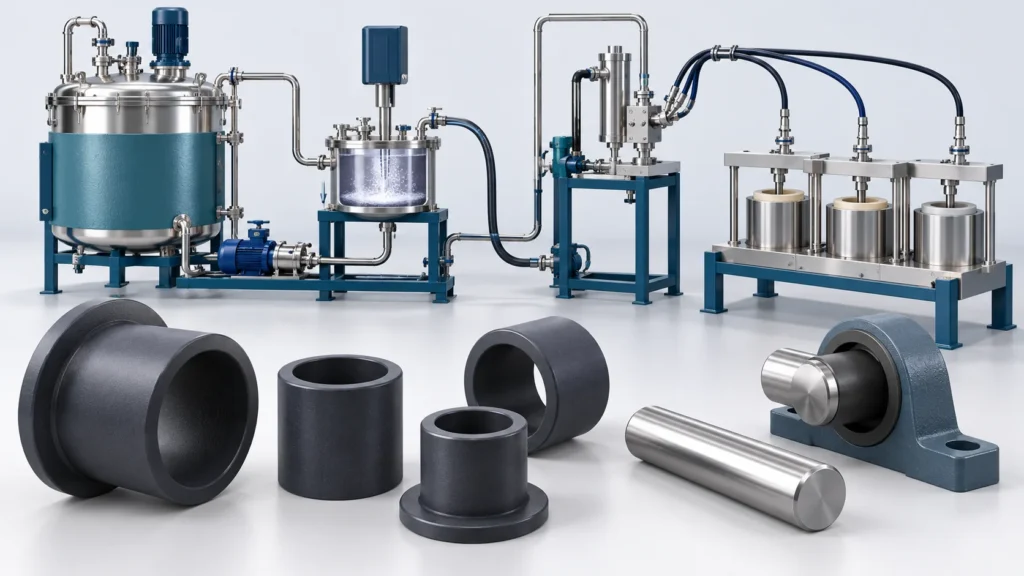
Preguntas frecuentes sobre la planificación de la producción
Selección, alcance de suministro y validación para esta ruta de producción.
Does the casting unit guarantee a friction coefficient or service life?
Does ultrasonic frequency establish stable suspension?
¿Qué información se necesita para una configuración preliminar?
Hablemos de sus objetivos de producción
Share the following with your production brief: Powder distribution/loading, monomer data, batch hold, bushing drawing, counterface, load/speed and exposure. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


