
Dual-Density Car Seat Foaming Line Solution
Define dual-density seat feed circuits, mixing-head routing and the zone interface before line selection.
Dual-Density Car Seat Foaming Line Solution
Dual-density seat production requires defined material recipes, regions and their bonding/transition. The stated primary material circuits and the mixing-head passages or chambers describe different parts of the system. Do not infer an additional material feed solely from a head label, or treat a ratio/index change as an unrestricted density-control method.
Alcance de suministro definido
Confirm the feed/return schematic, head model, active mixing sequence, robot and turntable. Single-shot versus sequential zone filling and mixed-model operation require representative material and mold trials.
Insumos para la selección del proceso
Seat zone map, recipes, feed/head schematic, mold and shot data, interface test requirements, mixed-model plan and shifts.
Equipment scope, retained factory interfaces and acceptance are agreed for the selected material and part. Confirm the feed/return schematic, head model, active mixing sequence, robot and turntable. Single-shot versus sequential zone filling and mixed-model operation require representative material and mold trials.
Dual-Density Car Seat Foaming Line Workflow
Define zones and materials → Confirm circuits and head → Dispense and mold → Inspect interface and output. Define preparation, filling, cure and output timing separately for the selected configuration.
Define zones and materials
Specify density and hardness separately and identify compatible recipes.
Confirm circuits and head
Map tanks, metering units, passages and active chamber routing.
Dispensar y moldear
Validate zone sequence, transitions and the cure process.
Parámetros técnicos
Configuración existente y referencias de ensayo. Los ajustes del equipo, los resultados del material y los resultados del conjunto terminado son independientes; aplique cada valor solo a su configuración y condiciones documentadas.
Composición de la línea
| Unidad de equipo | Cant. | Función |
|---|---|---|
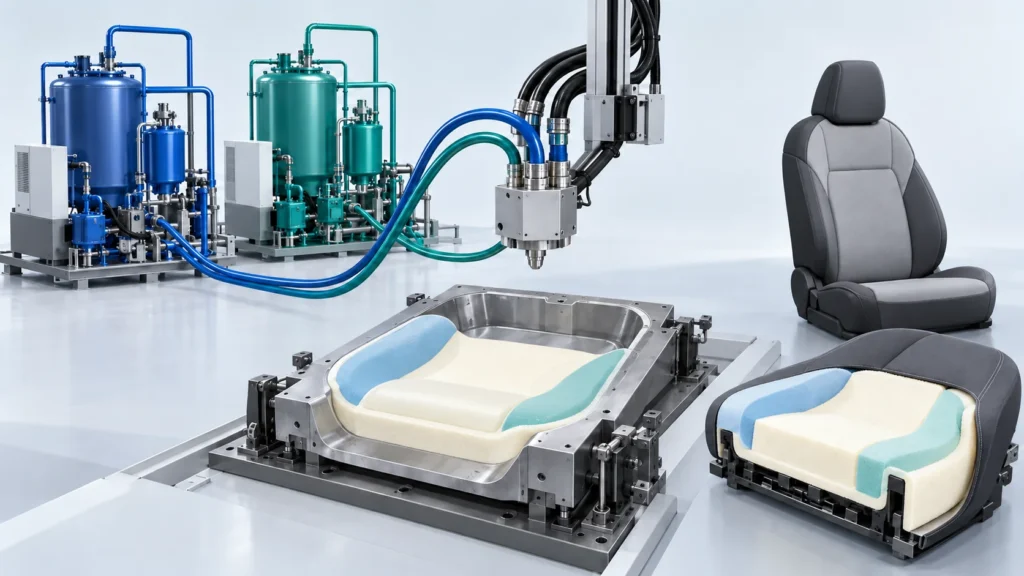
| 3-Component Dual-Density High-Pressure Foaming Machine | 1 unidad | 2 POLY + 1 ISO, four-component dual-chamber L-type mixing head, closed-loop metering |
| Robot de vertido | 1 unidad | Vertido automático siguiendo trayectorias definidas, distribución uniforme y posicionamiento preciso |
| Turntable Line | 1 unidad | Multi-station turntable, cyclic operation: pouring–foaming–mold opening–part removal |
| Sistema de control eléctrico | 1 unidad | Control inteligente por PLC con ajuste de parámetros, supervisión de estado y alarma de fallos |
Dual-Density High-Pressure Foaming Machine
| Parámetro | Valor |
|---|---|
| Modelo | HF-HPM-2A1B-DualDensityCarSeat |
| Component configuration | 3 components: 2 polyether polyol tanks + 1 isocyanate tank |
| Cabezal de mezcla | Four-component L-type high-pressure mixing head with dual mixing chambers |
| Metering method | 3 metering units; flow meters + VFDs control output flow and mix ratio |
| Density adjustment | Change recipe or mixing index for two dual-density process routes |
| Caudal de vertido | 50–1000 g/s |
| Precisión de dosificación | ≤ ±0,3 %, en todo el rango dinámico |
| Configuración de tanques | Independent temp control + circulation stirring for each tank |
| Control de temperatura | 20–45 ℃ |
| Presión de mezcla | 10–18 MPa |
| Sistema de limpieza | Purga de aire automática, sin disolventes |
| Potencia | 5,5–7,5 kW |
| Sistema de control | PLC + pantalla táctil + almacenamiento de múltiples fórmulas |
| Sistema de aplicación | Dual-density cold-cure / high-resilience flexible foam system |
| Garantía | 1 año |
| Certificación | CE, ISO9001 |
Dual-Density Foaming Process
| Elemento | Descripción |
|---|---|
| Component configuration | 2 polyether polyol tanks + 1 isocyanate tank |
| Mixing method | Four-component dual-chamber L-type mixing head, chambers adjusted independently |
| Metering control | 3 metering units with flow meters and VFDs |
| Density adjustment | Change recipe or mixing index to change foam density |
| Process routes | 2 density routes, switchable between soft layer and support layer |
| Mixed-line production | Front seat, rear seat and headrest on one line |
Equipamiento auxiliar para su línea de espumado
Las referencias de equipos se seleccionan según su proceso documentado. La dosificación principal, el suministro auxiliar y las rutas alternativas no constituyen un único paquete estándar.
Controles de proceso y verificaciones de aplicación
Evalúe estas funciones con el material, los moldes y el resumen de producción seleccionados. Los resultados de las piezas acabadas requieren su propia evidencia de aceptación.
Clear feed architecture
Separate primary components, metering circuits and head chambers in the configuration description.
Validated zone transition
Establish interface quality with the selected materials and mold.
Defined production basis
Balance cycle, molds, model changes and work schedule rather than combining headline values.
Proyectos relacionados
Estas son referencias de aplicación relacionadas. Compare el material, el proceso y los módulos entregados reales; las cifras de proyecto reportadas no son resultados de aceptación para otra línea.
Preguntas frecuentes sobre la planificación de la producción
Selección, alcance de suministro y validación para esta ruta de producción.
How do the three-component and four-component head descriptions relate?
Does changing index guarantee a second density?
¿Qué información se necesita para una configuración preliminar?
Obtenga una cotización gratuita
Share the following with your production brief: Seat zone map, recipes, feed/head schematic, mold and shot data, interface test requirements, mixed-model plan and shifts. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


