
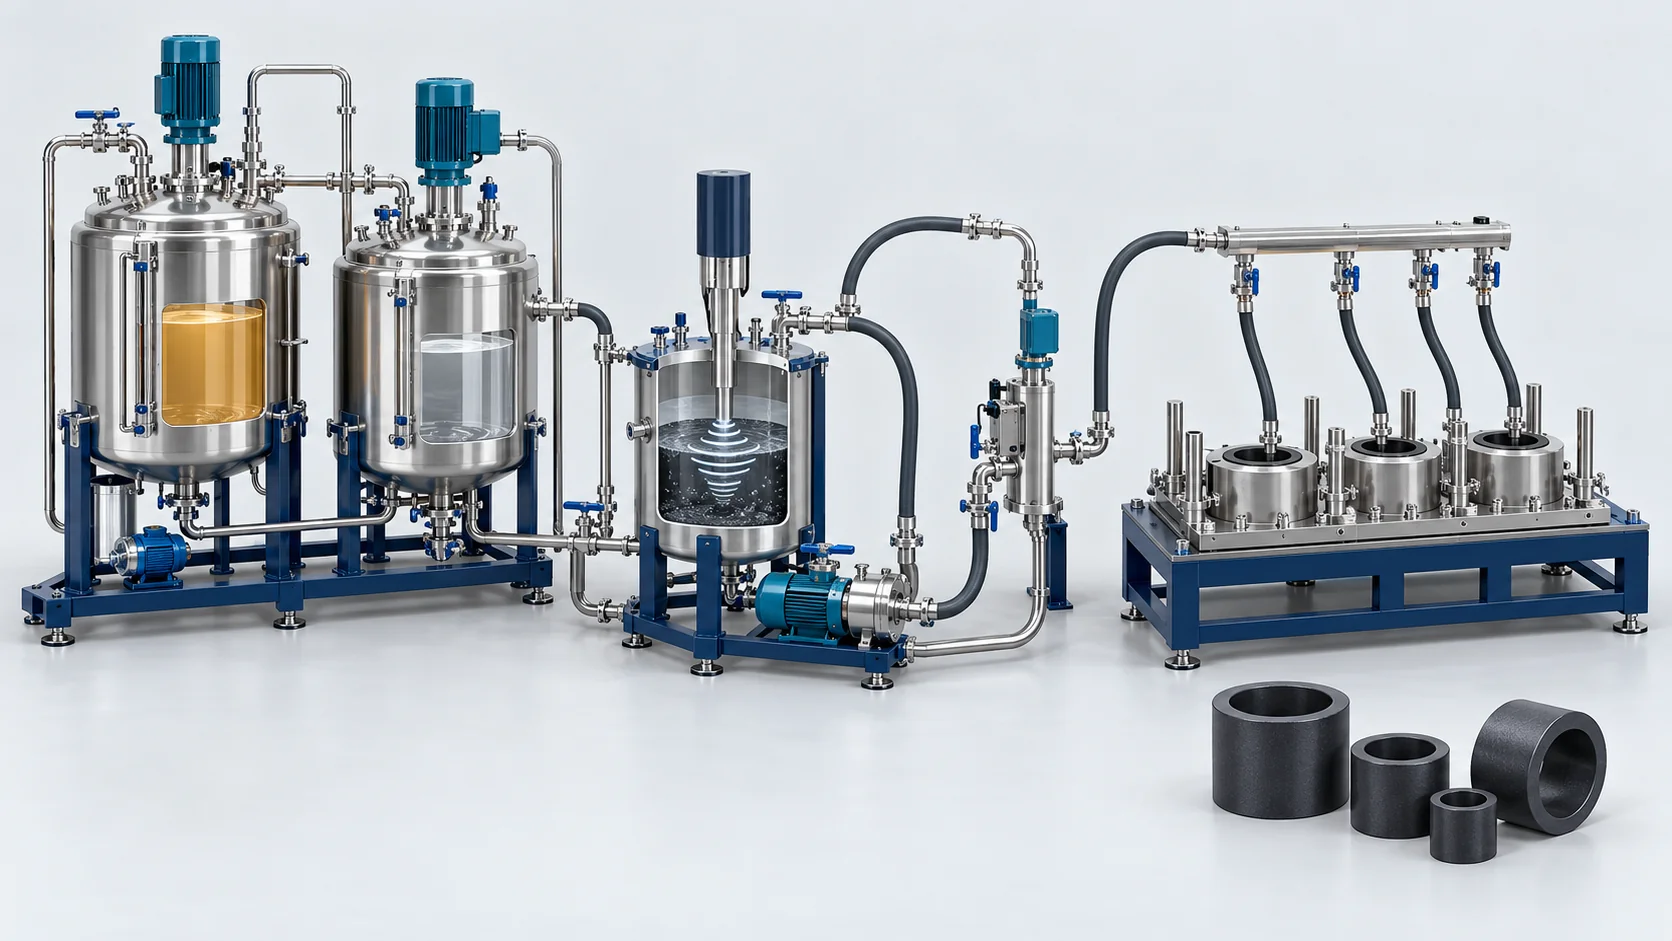
حل صب نايلون MC المعدل بـ MoS2
Configure additive dispersion, circulation and reactive MC Nylon casting for the selected modified bushing material.
Wear and Lubrication Process Engineering for Heavy Machinery Bearings
Modified nylon bushing production requires additive wetting, dispersion, suspension control and a compatible reactive casting process. Ultrasonic frequency and pump construction describe equipment functions; they do not establish friction coefficient, wear life or maintenance-free service for a bushing.
نطاق توريد محدد
Define additive preparation, thermal holding, recirculation, metering and tooling together. Powder size terminology must follow the actual distribution rather than treating micron-sized powder as submicron.
المدخلات لاختيار العملية
Powder distribution/loading, monomer data, batch hold, bushing drawing, counterface, load/speed and exposure.
Equipment scope, retained factory interfaces and acceptance are agreed for the selected material and part. Define additive preparation, thermal holding, recirculation, metering and tooling together. Powder size terminology must follow the actual distribution rather than treating micron-sized powder as submicron.
MoS2-Modified MC Nylon Casting Workflow
Characterize the formulation → Disperse and circulate → Meter and cast → Condition and evaluate. Define preparation, filling, cure and output timing separately for the selected configuration.
Characterize the formulation
Confirm monomer system, MoS2 size/loading and any other additive.
Disperse and circulate
Develop the wetting, dispersion and hold procedure for the actual powder.
القياس والصب
Validate material delivery and reaction in the selected bushing tool.
النطاق الهندسي للحل المرجعي
مراجع التكوين الحالي والاختبار. تُعد إعدادات المعدات ونتائج المواد ونتائج التجميع النهائي منفصلة؛ ويُطبَّق كل قيمة فقط على التكوين والظروف الموثقة الخاصة بها.
| المعامل | القيمة / الوحدة | التكوين / الظروف المطبَّقة |
|---|---|---|
| معدل تدفق الصب المستمر | 3.0 to 25.0 kg/min | Zirconia ceramic-lined positive displacement pump skid |
| Dynamic Friction Coefficient | 0.08 to 0.12 (Dry unlubricated friction) | ASTM G99 pin-on-disk test under 35 MPa contact pressure |
| Ultrasonic Cavitation Frequency | 20 kHz (Continuous acoustic horn) | High-power ultrasonic generator inside molten vessel |
| Supported MoS₂ Powder Loading | 1.0% to 6.0% by weight | Sub-micron 1– 3 µm particle size de-agglomerated |
| Grease-Free Bushing Wear Life | Greater than or equal to 8,000 Hours | Verified radial wear under 0.1 mm in abrasive dust service |
| Annealing Oil Bath Temperature | Up to 150°C | Multi-zone thermal oil immersion tank relieving stress |
المعدات الأساسية لهذا الحل
تُختار مراجع المعدات وفق عمليتها الموثّقة. القياس الرئيسي للجرعات والإمداد المساعد والمسارات البديلة ليست حزمة قياسية واحدة.
ضوابط العملية وفحوص التطبيق
قيّم هذه الوظائف باستخدام المادة والتجهيزات القالبية الموجزة الإنتاجية المختارة. تتطلب نتائج الأجزاء النهائية أدلة قبول خاصة بها.
Additive-specific preparation
Select dispersion and circulation after material trials and endpoint evaluation.
Compatible material circuits
Review filled-material wear, seals, thermal control and cleaning.
Duty-specific tribology
Separate equipment functions from friction and endurance measurements.
مشاريع ذات صلة
هذه مراجع تطبيقية ذات صلة. قارن المادة الفعلية والعملية والوحدات المسلّمة؛ فأرقام المشاريع المبلَّغ عنها ليست نتائج قبول لخط آخر.
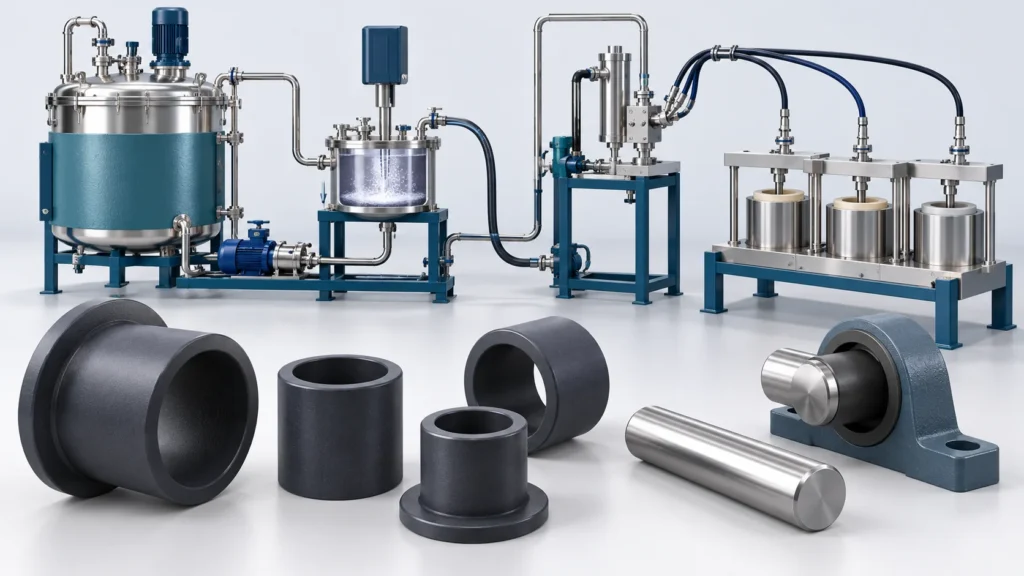
الأسئلة الشائعة حول تخطيط الإنتاج
الاختيار ونطاق التوريد والتحقق لهذا المسار الإنتاجي.
Does the casting unit guarantee a friction coefficient or service life?
Does ultrasonic frequency establish stable suspension?
ما المعلومات المطلوبة لإعداد تكوين أولي؟
ناقش أهدافك الإنتاجية
Share the following with your production brief: Powder distribution/loading, monomer data, batch hold, bushing drawing, counterface, load/speed and exposure. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


