
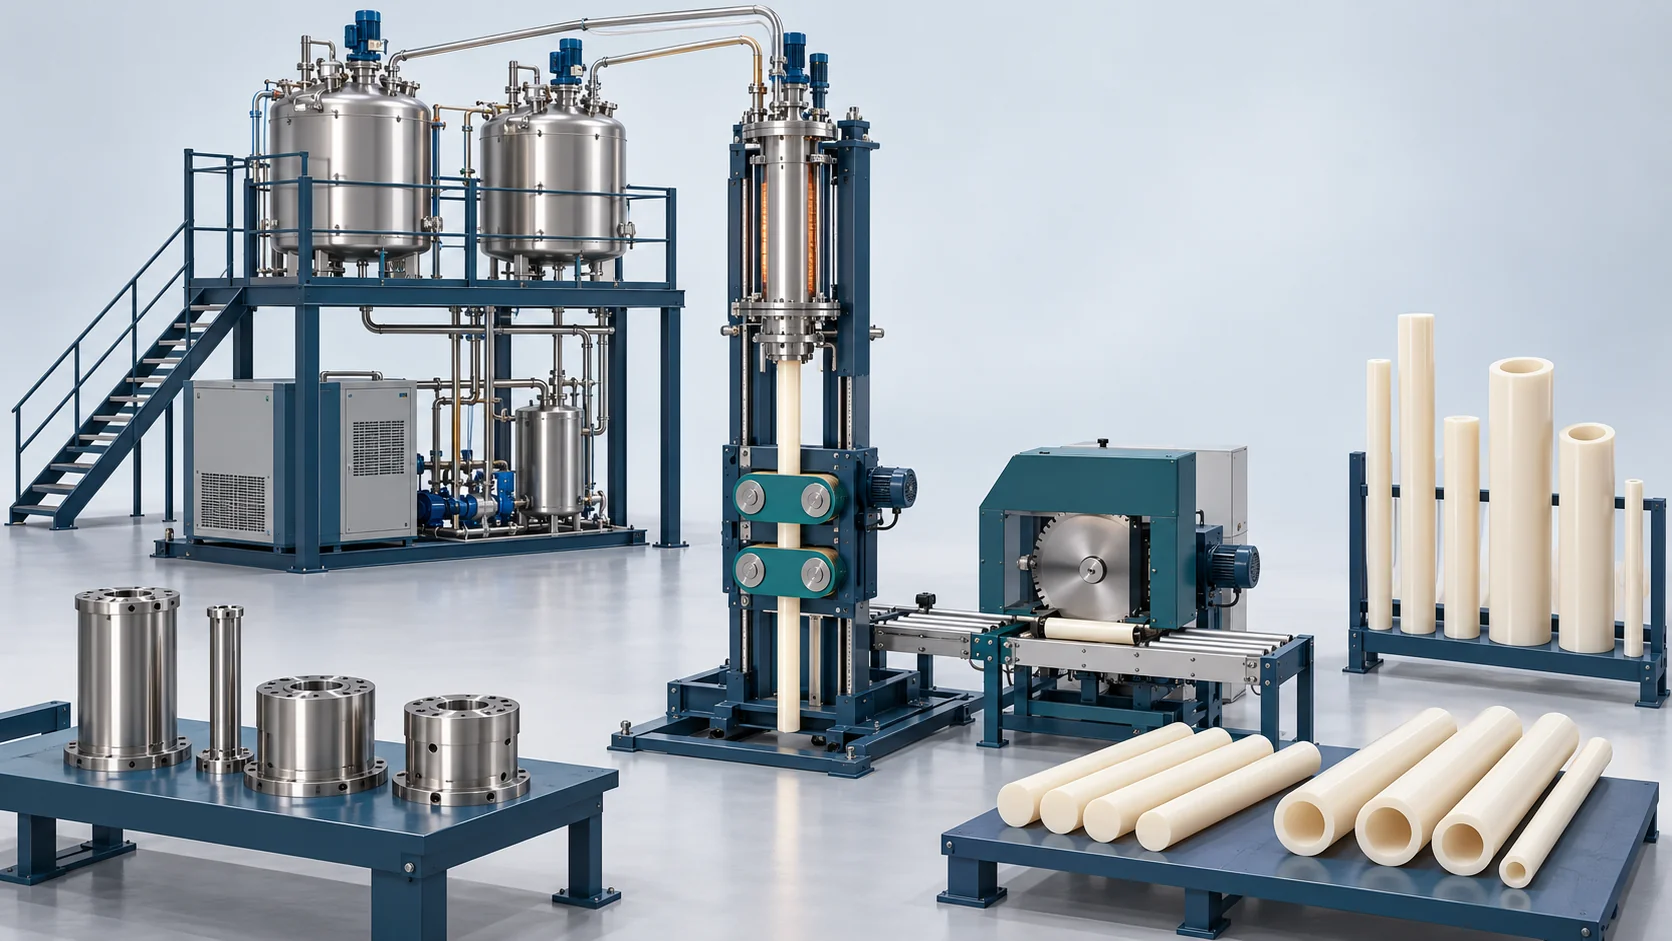
حل الصب المستمر لقضبان نايلون MC
Coordinate continuous MC Nylon rod or tube casting with reaction tooling, haul-off and synchronized cutting.
Unbroken Vertical Pultrusion for Large-Diameter Structural & Insulating Stock
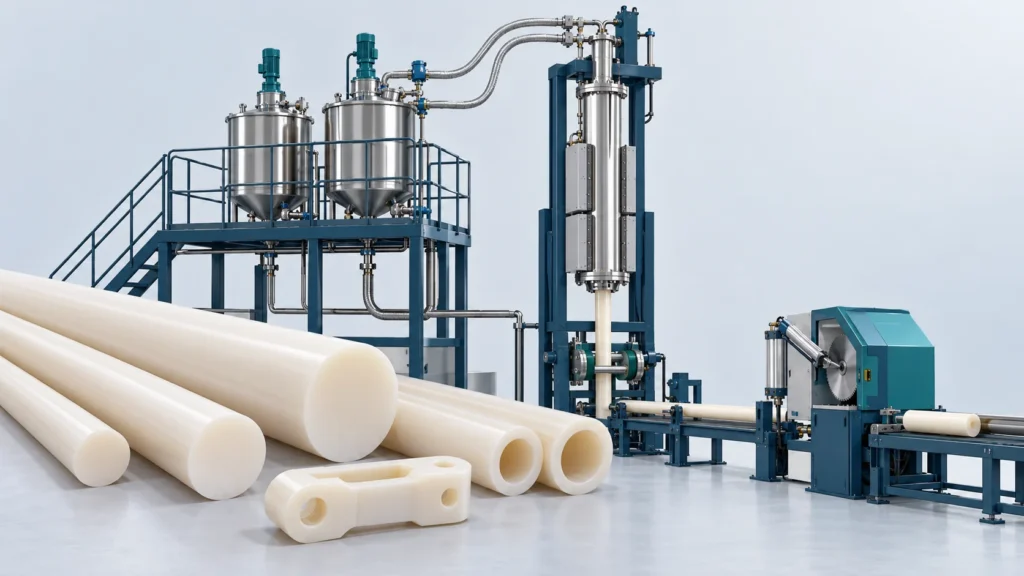
Continuous cast-nylon stock links prepared monomer delivery to a heated forming die, controlled polymerization, pulling and cutting. Solid rods and hollow tubes use different tooling and stability checks. Electrical properties and molecular-weight statements require material measurements separate from line speed or pump capacity.
نطاق توريد محدد
Define the die/mandrel, thermal controls, haul-off, cutting and downstream conditioning. Annual output must use a stated section, production schedule, availability and accepted yield.
المدخلات لاختيار العملية
Rod/tube diameters and wall, formulation, length/cutoff needs, work schedule, downstream machining and electrical tests.
Equipment scope, retained factory interfaces and acceptance are agreed for the selected material and part. Define the die/mandrel, thermal controls, haul-off, cutting and downstream conditioning. Annual output must use a stated section, production schedule, availability and accepted yield.
Continuous MC Nylon Rod Casting Workflow
Prepare the monomer system → Feed the forming tool → Polymerize and haul off → Cut, condition and inspect. Define preparation, filling, cure and output timing separately for the selected configuration.
Prepare the monomer system
Confirm formulation, dehydration and conditioned feed.
Feed the forming tool
Coordinate delivery with the selected solid-rod or hollow-tube tooling.
Polymerize and haul off
Validate thermal behavior, release and stable pulling for the section.
النطاق الهندسي للحل المرجعي
مراجع التكوين الحالي والاختبار. تُعد إعدادات المعدات ونتائج المواد ونتائج التجميع النهائي منفصلة؛ ويُطبَّق كل قيمة فقط على التكوين والظروف الموثقة الخاصة بها.
| المعامل | القيمة / الوحدة | التكوين / الظروف المطبَّقة |
|---|---|---|
| Continuous Finished Diameter Range | Ø 50 mm to Ø 200 mm (Solid rod stock) | Precision chrome-plated continuous crystallization dies |
| Hollow Tube Diameter Capability | Ø 100 mm to Ø 300 mm outer diameter | Internal water-cooled sizing mandrels for heavy-wall tubes |
| قوة الانهيار العازل | Greater than or equal to 30.0 kV/mm | GB/T 1408.1 testing on cured railway insulation stock |
| Polymer Molecular Weight (Mw) | 70,000 to 100,000 | Viscometric measurement on in-die polymerized PA6 |
| Continuous Downward Pull Speed | 50 to 300 mm/min | Multi-track servo caterpillar haul-off with speed encoder |
| Annual Line Production Capacity | Up to 1,500 Metric Tons/year | Uninterrupted 24/7 continuous vertical casting operation |
المعدات الأساسية لهذا الحل
تُختار مراجع المعدات وفق عمليتها الموثّقة. القياس الرئيسي للجرعات والإمداد المساعد والمسارات البديلة ليست حزمة قياسية واحدة.
ضوابط العملية وفحوص التطبيق
قيّم هذه الوظائف باستخدام المادة والتجهيزات القالبية الموجزة الإنتاجية المختارة. تتطلب نتائج الأجزاء النهائية أدلة قبول خاصة بها.
Section-specific tooling
Differentiate solid-rod and hollow-tube designs and process limits.
Coupled feed and haul-off
Balance material delivery, reaction and pulling rather than using independent maxima.
Defined material measurements
Report dielectric and molecular-weight results with the specimen and actual measurement method.
مشاريع ذات صلة
هذه مراجع تطبيقية ذات صلة. قارن المادة الفعلية والعملية والوحدات المسلّمة؛ فأرقام المشاريع المبلَّغ عنها ليست نتائج قبول لخط آخر.
الأسئلة الشائعة
Does line speed establish annual tonnage?
How should the molecular-weight reference be interpreted?
ما المعلومات المطلوبة لإعداد تكوين أولي؟
ناقش أهدافك الإنتاجية
Share the following with your production brief: Rod/tube diameters and wall, formulation, length/cutoff needs, work schedule, downstream machining and electrical tests. Our team will reply within one business day. Once requirements are clear, we provide a preliminary proposal within two business days.


