
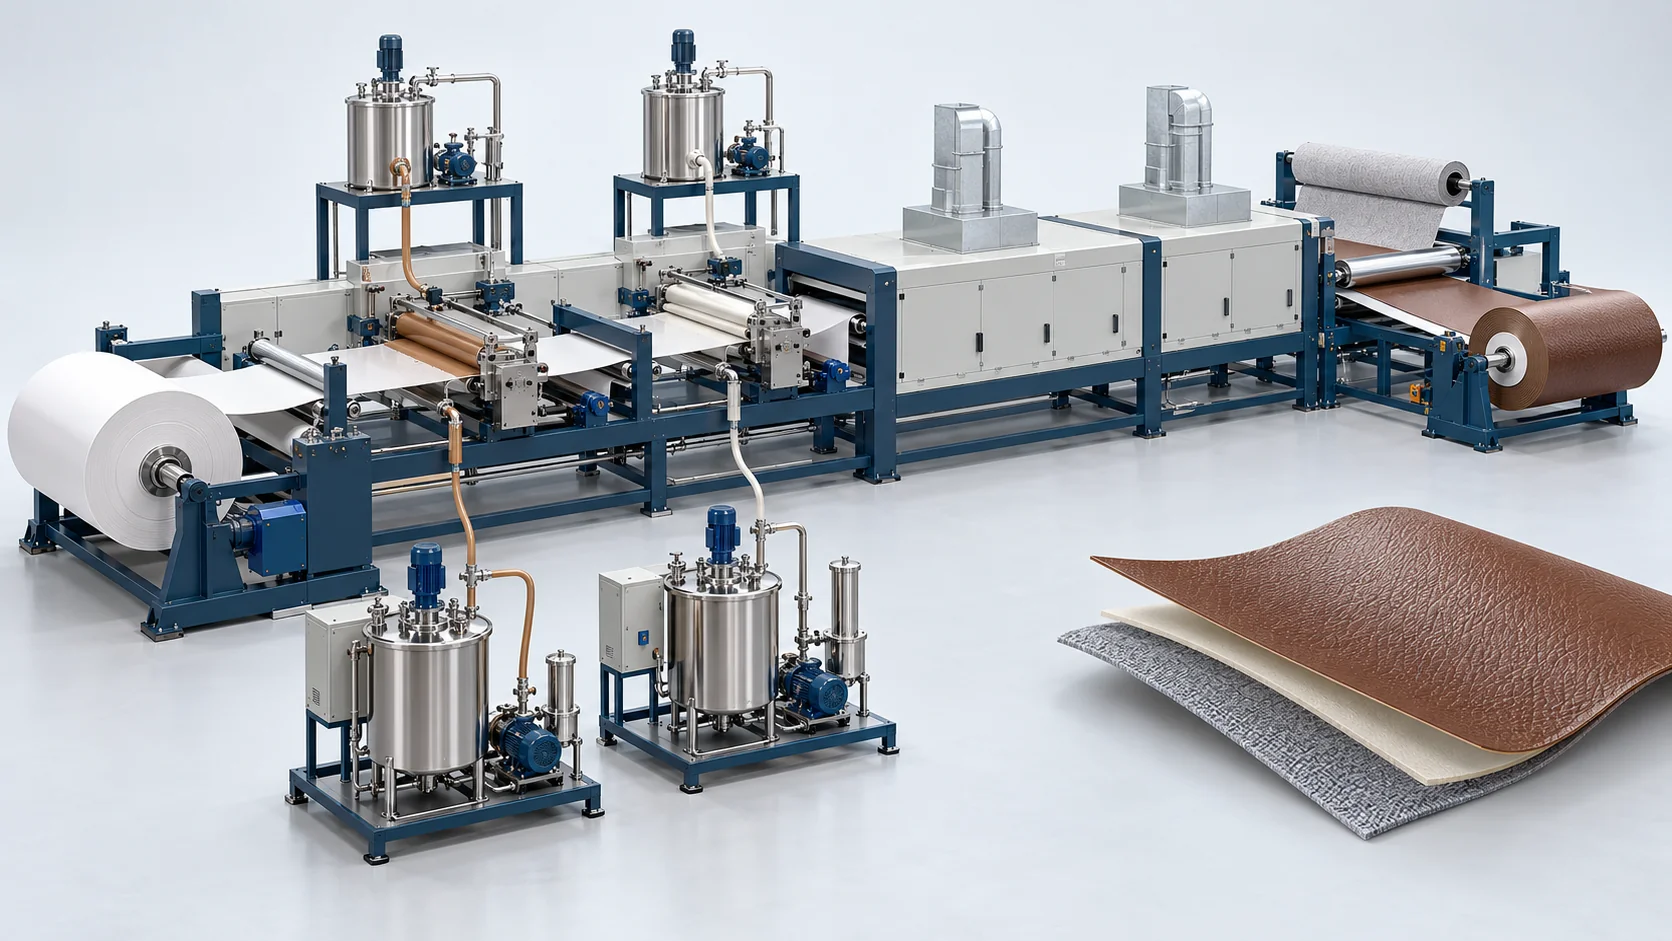
خط الطلاء بالنقل لـ PU | الجلد في العملية الجافة
إمداد الطبقة العليا واللاصق على ورق الفصل، مع تجفيف وتصفيح منسّقين للجلد الصناعي PU بالعملية الجافة.
معدل تدفق التصريف
Topcoat: 20–100 kg/h; Adhesive: 30–120 kg/h
نسبة الخلط
Adhesive 100:3 to 100:10 (By weight)
مرجع الدقة
±0.3% (Continuous mass flow feedback on adhesive stream)
ضغط التشغيل
0.3 to 0.5 MPa (Slot die and adhesive line)
Precision Dry-Process Transfer Coating for Performance Footwear
إمداد الطبقة العليا واللاصق على ورق الفصل، مع تجفيف وتصفيح منسّقين للجلد الصناعي PU بالعملية الجافة.
Release-paper topcoat delivery, proportioned adhesive supply, drying and lamination are coordinated for dry-process PU synthetic leather. Topcoat and adhesive circuits have different chemistry, delivery rates and cleaning requirements.
Release paper, fabric, resin formulation, ovens, solvent recovery and winding scope are specified for the line. Dry-process describes the manufacturing route; it does not itself mean solvent-free operation.
رسم تصوري: رسم توضيحي مُولَّد لمناقشة العملية؛ وليس صورة للآلة المحددة أو لمنشأة عميل أو لمشروع مُسلَّم.
تدفق المواد ومبدأ العمل
Prepare Release Paper and Topcoat
Select the release paper, resin and topcoat delivery and coordinate the coating-head settings with the web.
Coat and Dry
Run the specified topcoat and oven stages for the actual resin chemistry and line speed.
Apply Adhesive and Laminate
Meter the selected adhesive and coordinate lamination with the backing and thermal window.
Wind and Inspect Leather
Receive the finished web and evaluate thickness, appearance, bonding and other agreed material requirements.
هل تحتاج إلى عرض سعر لهذه المعدات؟
اطلب عرض سعرالطراز والمعايير الفنية
The listed references describe web handling, topcoat and adhesive delivery, coating and lamination. Web tension, coating thickness and line speed require defined operating conditions. Flexibility, peel strength and emissions are finished-material and process acceptance items.
| المعلمة الفنية | HF-DPC180-TR |
|---|---|
| المكوّنات | Topcoat 1 Component + Adhesive 2 Components (Base + Crosslinker) |
| نطاق الإخراج | Topcoat: 20–100 kg/h; Adhesive: 30–120 kg/h |
| نطاق نسبة الخلط | Adhesive 100:3 to 100:10 (By weight) |
| مرجع الدقة | ±0.3% (Continuous mass flow feedback on adhesive stream) |
| مصدر الطاقة | 380 فولت، ثلاثي الأطوار، 50 هرتز (اختياري مخصص 440 فولت/480 فولت 60 هرتز) |
| ضغط التشغيل | 0.3 to 0.5 MPa (Slot die and adhesive line) |
| سعة الخزان / القادوس | Day tanks: 2 x 200 L (Stainless steel with pneumatic stirrers) |
| الوزن | 18,500 kg (Combined coater, ovens, laminator, and rewinder) |
| الأبعاد (الطول×العرض×الارتفاع) | 58,000 mm x 3,600 mm x 3,400 mm (Total line footprint) |
الميزات الرئيسية للمعدات
Topcoat supply, proportioned adhesive stream, coating dies, ovens, laminator and winding interfaces; release paper, fabric, resin chemistry and solvent recovery are specified separately.
Controlled Web Handling
Coordinate release-paper tension and line ramps with the selected web, coating load and winding arrangement.
Configured Coating Application
Select the coating head and operating window for the resin, target thickness and web width. Measure cross-web thickness on the resulting layer.
Drying and Lamination Interfaces
Coordinate drying, adhesive delivery and lamination with the resin chemistry, backing and thermal window.
Finished-Leather Evaluation
Define flexing, peel, appearance and any emissions requirements on representative leather specimens with the agreed conditioning and test methods.
ناقش تكوين معداتك
شارك معلومات منتجك والمواد والتجهيزات القالبية ومتطلبات الإنتاج كي نتمكن من مراجعة المعدات والواجهات لمشروعك.
الأسئلة الشائعة
What is the difference between topcoat and adhesive supply?
Does dry-process mean solvent-free?
How are tension and thickness references accepted?
How are cold flex and peel requirements defined?
هل أنت مستعد لمناقشة مشروعك؟
تواصل مع فريقنا


